Leave Your Message
Top-tier raw material powders and extracts customized for UK brand specifications.
Analyzing the commercial demand, technological evolution, and application scenarios in the United Kingdom.
In recent years, the United Kingdom has witnessed an unprecedented surge in health and wellness awareness. Consumers in major metropolitan hubs like London, Manchester, Birmingham, and Edinburgh are actively seeking clean-label, plant-based nutritional alternatives. Superfruit powders—ranging from high-antioxidant blueberry and mulberry extracts to nutrient-dense tropical options—have transitioned from niche health food stores to mainstream supermarkets and online direct-to-consumer (DTC) brands.
As a leading superfruit powder factory supplying the United Kingdom, we understand that British buyers prioritize traceability, purity, and certification standard alignment. The modern UK consumer demands products that support immune health, cognitive function, and metabolic wellness without synthetic additives. This shift has placed immense pressure on UK supplement brands to partner with global manufacturers capable of delivering high-purity, standardized botanical extracts.

Our raw materials are engineered to suit a variety of finished product formats popular in the British Isles:
Instant-dissolving superfruit powders like blueberry and mulberry are widely used by UK beverage manufacturers to create ready-to-drink functional juices and custom smoothies for urban wellness bars.
High-street retailers and digital brands utilize our premium extracts to formulate targeted capsules addressing cognitive clarity, skin health, and joint support.
British breakfast brands incorporate freeze-dried superfruit powders into instant oatmeals, mueslis, and healthy snacks to enhance both natural color and nutritional profiles.
Your Trusted Global Supply Chain Partner for Natural Raw Materials
Shaanxi Yuantai Biological Technology Co., Ltd. was established in 2014. Its headquarter is located in Xi'an and its factory is located in Weinan Economic and Technological Development Zone. The factory covers an area of 10000+㎡.
At present, the company's main categories include: capsules, granules, tablets, solid beverages, soft candies and other OEM categories. YTBIO has 10 years of production experience in the raw material field. The main categories include: herbal extracts, nutritional supplements, organic extract raw materials and cosmetic raw materials.
YTBIO is a comprehensive health food manufacturer. With its understanding of the raw material industry and products, it uses industry experience to provide compounding solutions from raw materials to finished products, and supports professional solutions in product packaging, flexible application of ingredients, and product label design. In addition, we are also committed to developing new products to provide customers with more product and formula options to meet the various needs of different customers for products.
Rigorous quality control and advanced extraction technology to guarantee product stability and safety.

YTBIO's production facilities and equipment meet national standards, and the production process is strictly carried out in accordance with GMP requirements. The raw materials meet national standards, and after comprehensive inspection and quality control, the production process is strictly carried out in accordance with scientific production process to ensure the safety, stability and effectiveness of the products.
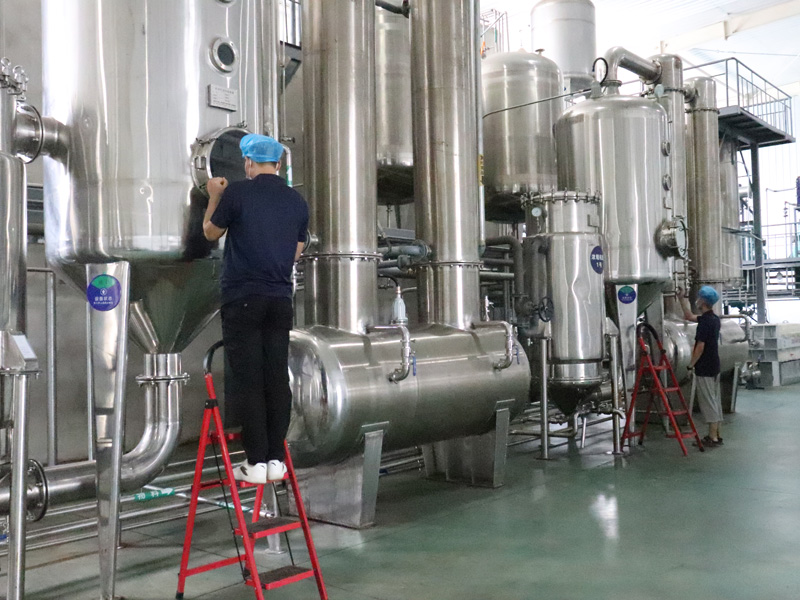
The factory has standardized R&D rooms and inspection rooms, and a 100,000-level GMP purification workshop. Using professional production experience, leading equipment, and professional technology, production is carried out in accordance with standardized processes. Strict standards have been set for every link in the production process.
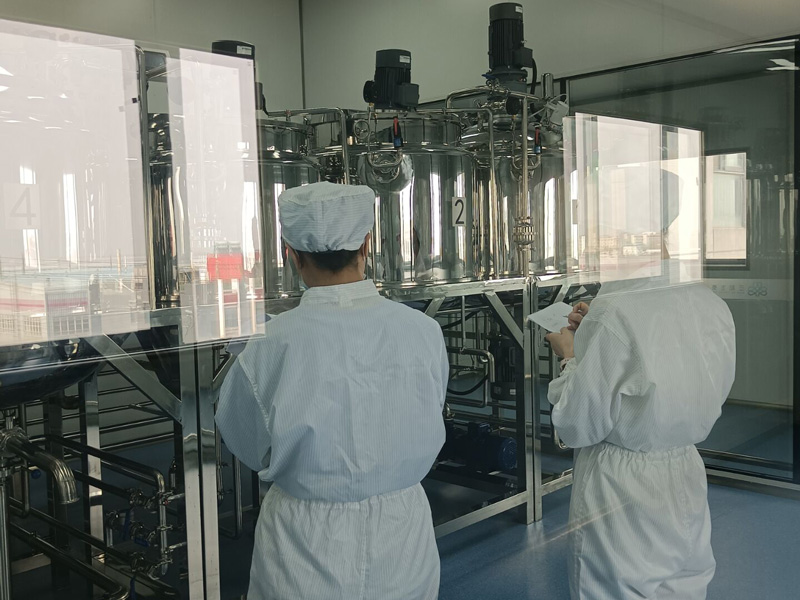
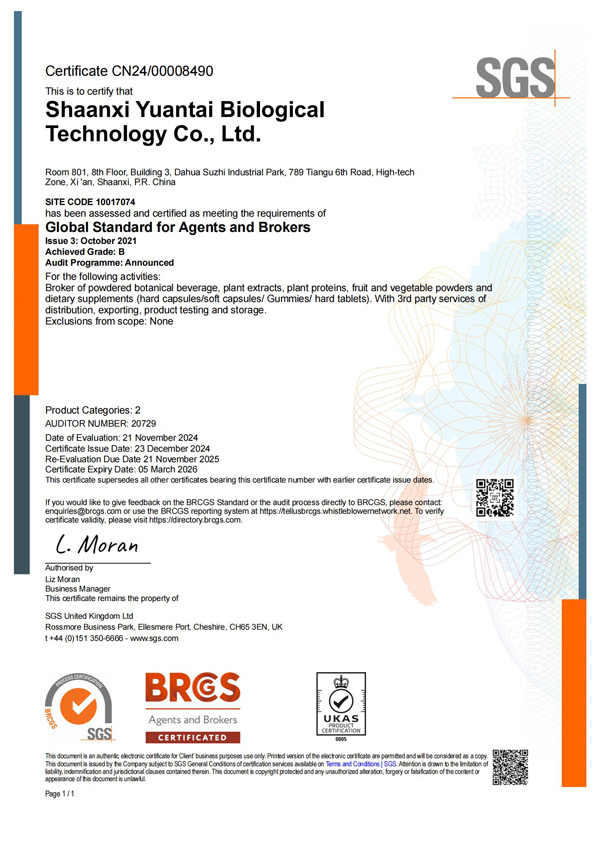
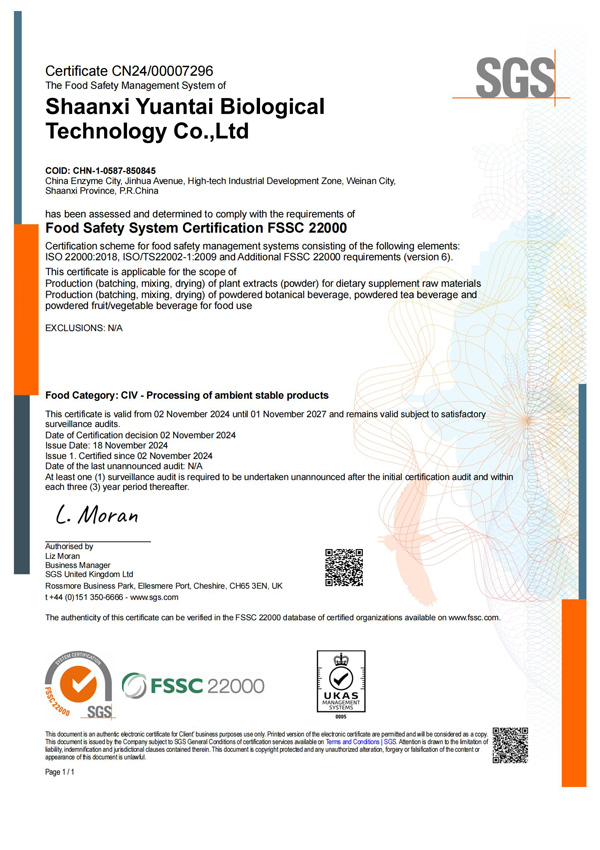
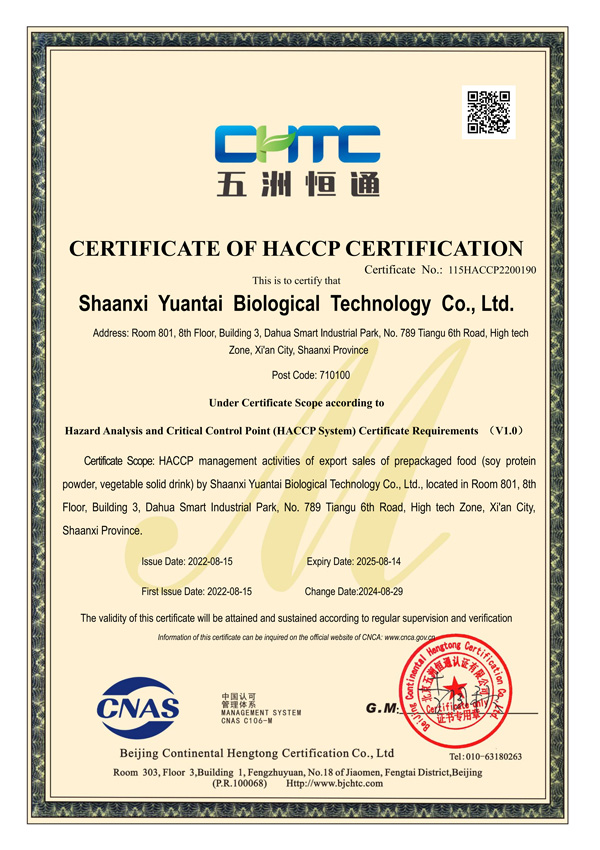
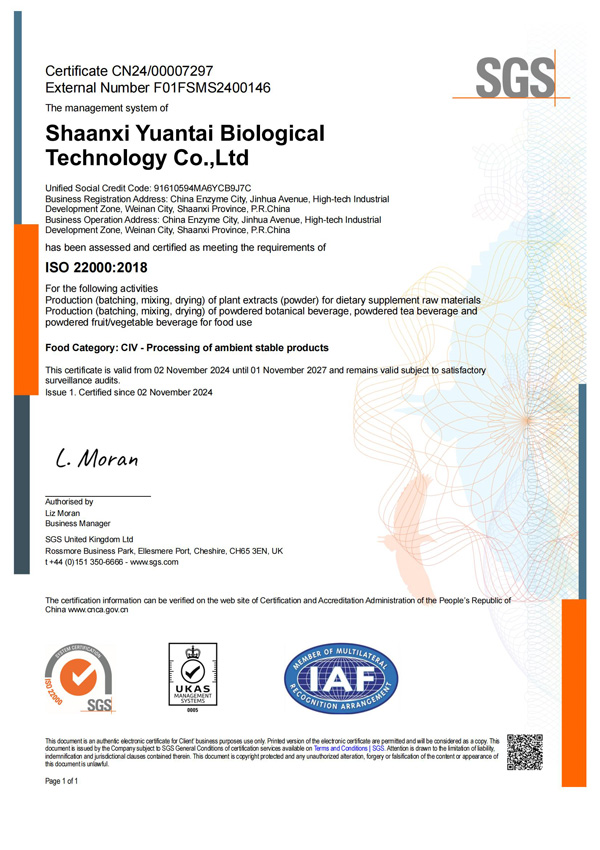
In the 10 years of development, the company has continuously improved its corporate management level, strengthened quality management, managed in accordance with the requirements of the international standardized quality management system, and passed a number of certifications to promote rapid development.
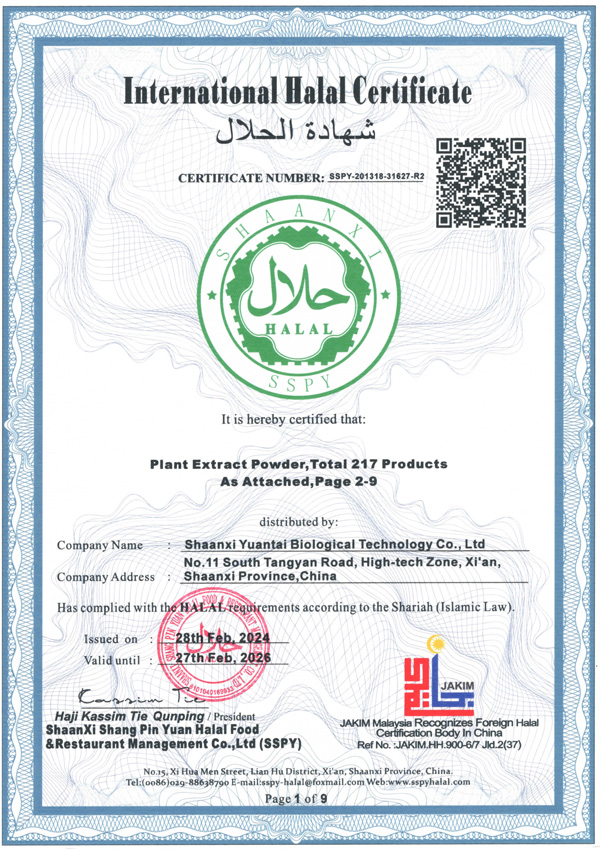
To ensure product quality and production process standards, we have passed cGMP, FSSC22000, BRC, HACCP, ISO9001, ISO22000, HALAL, KOSHER, FDA, and EU & US organic certifications.

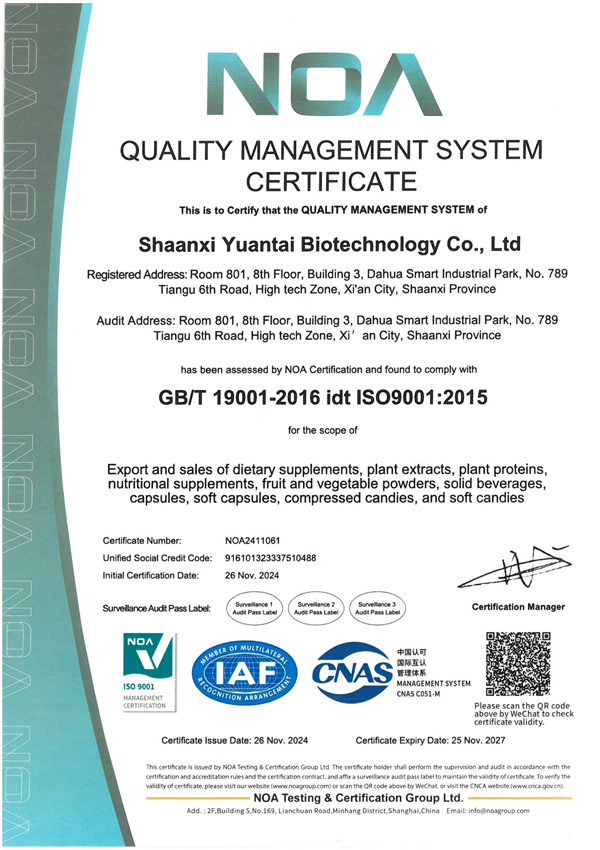
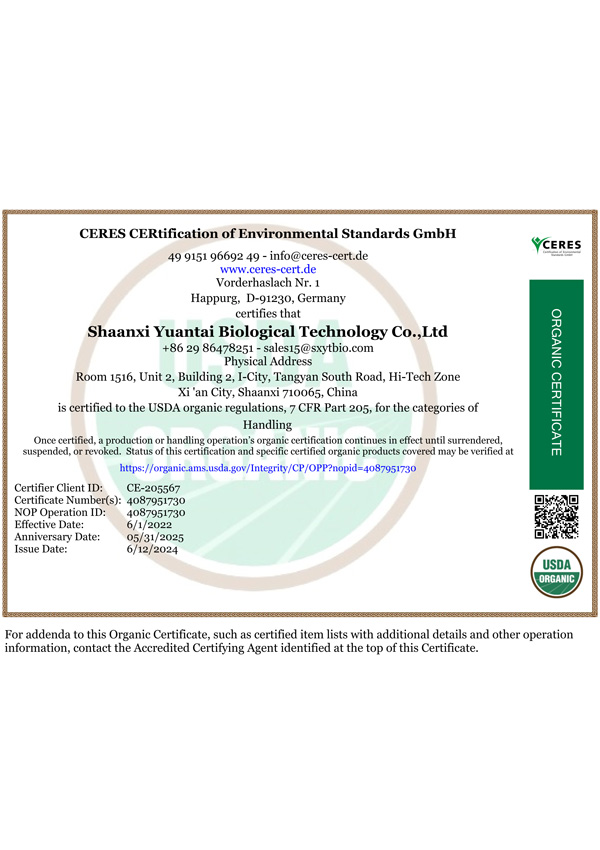
From raw materials and formulation design to custom packaging and labeling for UK private labels.
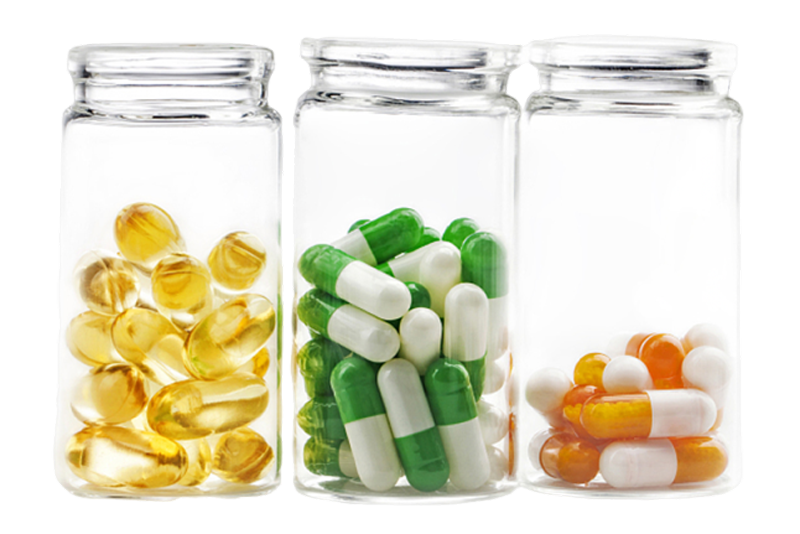
We provide finished packaging or production of separate operations, including raw material weighing, homogenizing, and encapsulation.
Shell Materials: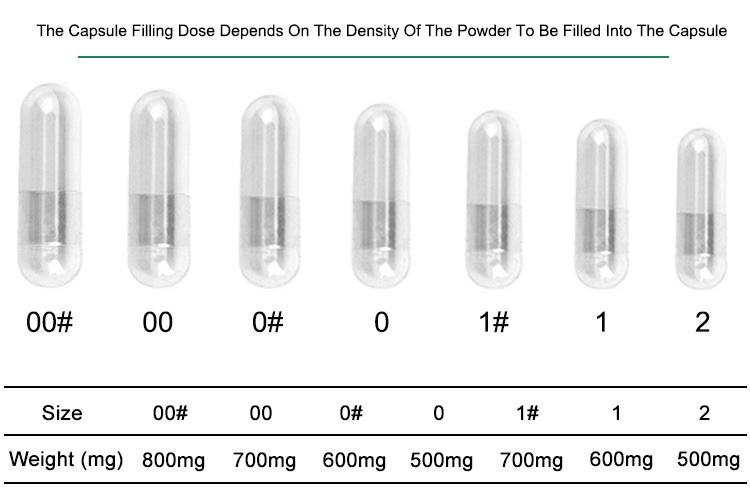
High-precision compression technology for stable dosage and optimal dissolution profile.
Specifications: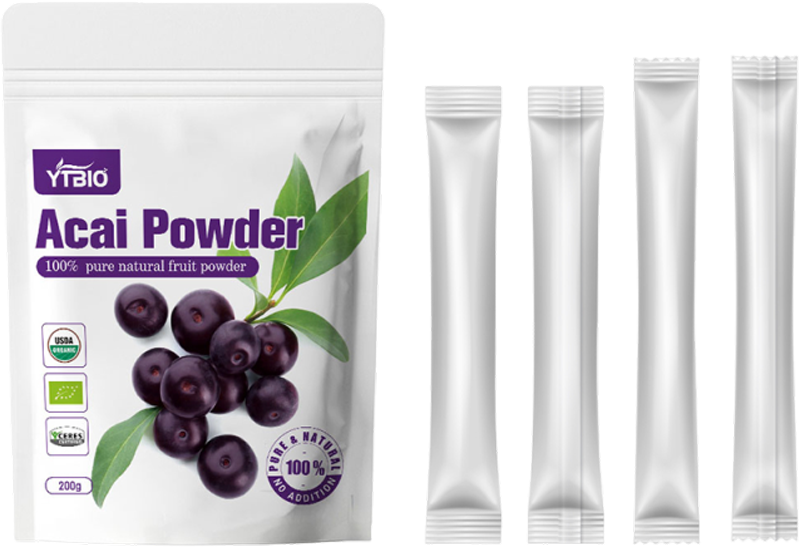
Production of instant teas, granular beverages, and nutrient powder blends packed directly for distribution.
Packaging & Flavors:We use the highest quality plant raw materials from reliable, audited suppliers. By producing and processing in our own factory, we provide a seamless one-stop service. We extract and process with high technical standards to retain the highest quality active ingredients of raw materials, ensuring that every batch of capsules, tablets, and solid drinks meets the strict demands of the UK and global health sectors.

Explore our full range of high-purity powders manufactured for British health brands and distributors.


